What Should a Bag Hardware Technical Drawing Include?
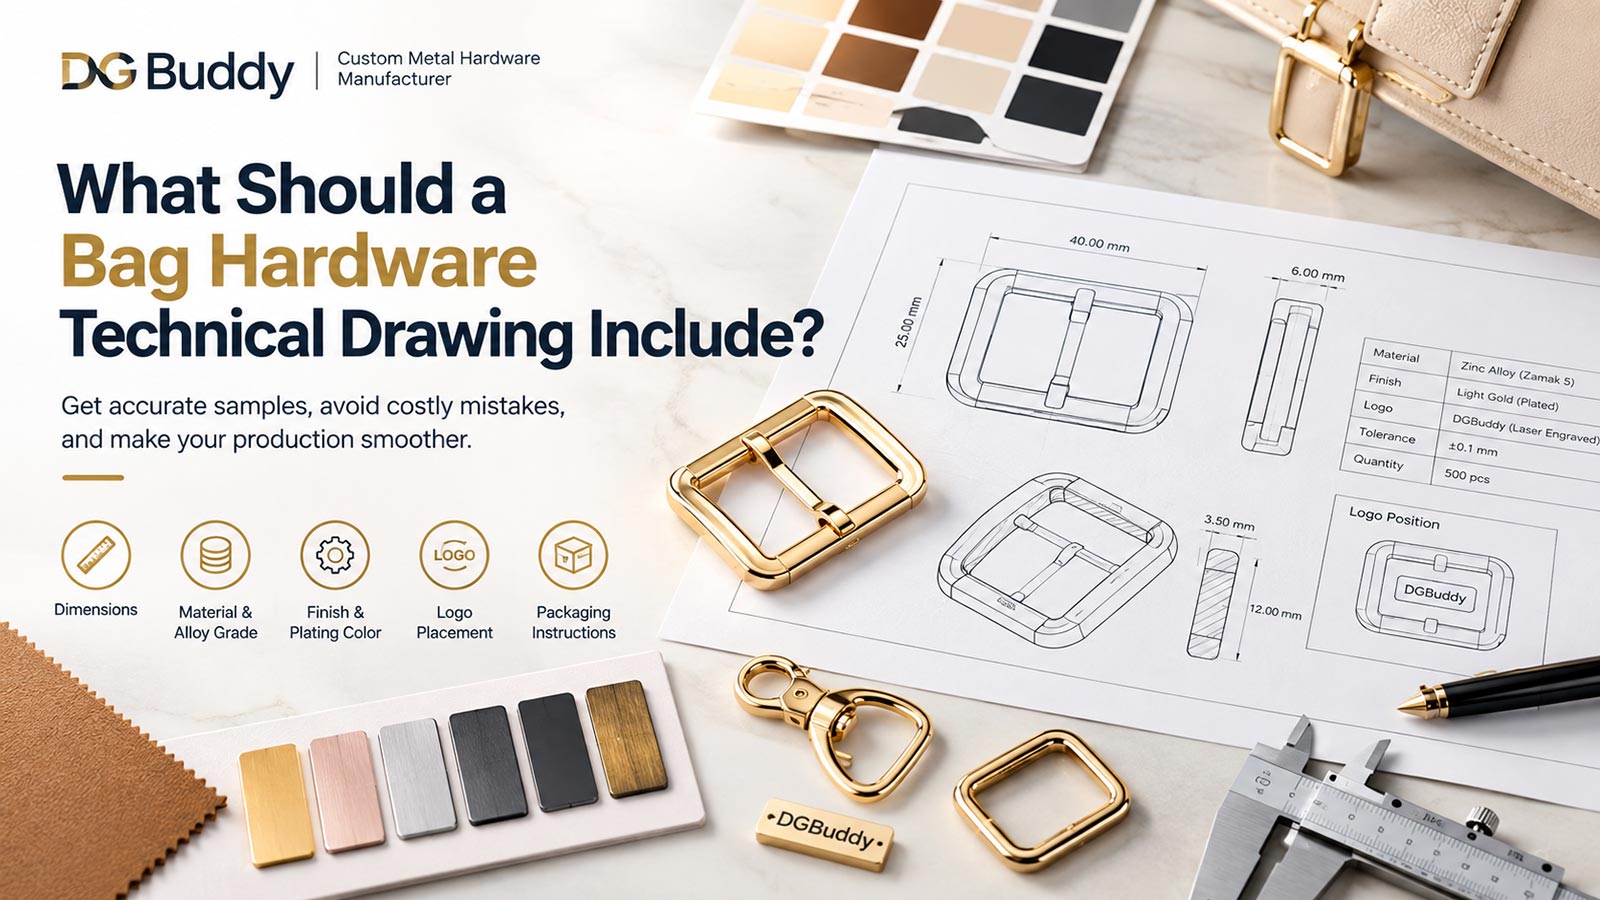
Every delay we see in handbag hardware production traces back to the same root cause: an incomplete bag hardware technical drawing. A buyer sends a sketch or a reference photo, the factory fills in the blanks with assumptions, and three weeks later the sample doesn’t match what the brand had in mind. A complete drawing removes the guesswork and gets you an accurate quote on the first try.
Quick Answer
A production-ready bag hardware technical drawing should include overall dimensions, material and alloy grade, wall thickness, hole diameter and position, post length, assembly direction, surface finish, plating color, logo placement, critical dimension tolerances, functional requirements, and packaging instructions. Missing any of these forces the factory to guess, which usually means a wrong first sample.
Key Takeaways
- A usable drawing needs 12 core data points, not just a shape sketch.
- Material and alloy grade change tooling cost, weight, and finish options.
- Hole position and post length errors are the single biggest cause of failed hardware fitting.
- Tolerances should be marked only on dimensions that actually affect function or assembly.
- Plating color references should use a physical sample or Pantone code, not a screen color.
- Packaging notes belong on the drawing, not in a separate email that gets lost.
Table of Contents
- Overall Dimensions and Product Silhouette
- Material and Alloy Specification
- Wall Thickness and Structural Details
- Hole Diameter, Position, and Post Length
- Assembly Direction
- Surface Finish and Plating Color
- Logo Placement and Branding Details
- Critical Dimension Tolerances
- Functional and Performance Requirements
- Packaging Requirements
- 2D Drawing vs 3D CAD vs Physical Sample
- Pros and Cons of Drafting Your Own Drawing
- Common Mistakes in Hardware Drawings
- Factory Expert Tips
- Expert Recommendation
- FAQ
Overall Dimensions and Product Silhouette
The drawing must state every outer dimension of the part – length, width, height, and any radius or angle that defines the silhouette. For a buckle, that means outer frame size and bar width; for a logo plate, overall footprint and edge profile.
Dimensions should be given in millimeters, since that is the working unit for most handbag hardware specifications in Chinese manufacturing. A drawing that mixes inches and centimeters without labeling units is a common source of first-sample errors, particularly when a design file is passed between a brand’s design team and a sourcing agent before it ever reaches the factory.
Material and Alloy Specification
State the base material by name, not by appearance. “Gold color” describes a finish, not a material – the drawing needs to specify zinc alloy, brass, or stainless steel, and ideally the alloy grade within that family.
Zinc alloy, commonly called Zamak, remains the default choice for die-cast handbag hardware because it captures fine detail at a manageable tooling cost. Our own zinc alloy hardware guide breaks down the differences between Zamak 2, 3, and 5, which matters because Zamak 5 handles daily strap tension better than Zamak 3 at a small cost premium. Brass, by contrast, is usually stamped or machined rather than die-cast, so it suits simpler geometries with a warmer, denser finish.
What Determines the Right Alloy for a Given Part?
What: Zamak 3 and Zamak 5 cover roughly 80% of fashion handbag hardware, while brass and 304 stainless steel are reserved for load-bearing or unplated “living finish” applications. Why: alloy choice affects casting detail, tensile strength, and how well the part accepts electroplating. How: specify the alloy family on the drawing and let the factory confirm the exact grade based on part geometry and expected load – a die-cast turn lock and a wire-formed D ring rarely use the same specification even when they look similar on paper.
Wall Thickness and Structural Details
Wall thickness controls both the strength and the weight of a die-cast part. A 2.5mm wall on a small buckle body behaves very differently under load than a 1.2mm wall, even when the outer dimensions are identical on the drawing.
For hollow or formed components such as rings and chain links, note the wire diameter as well as the wall thickness of any stamped section. Two parts with the same outer profile can have very different load capacity if internal thickness isn’t specified – this is one of the most common corners cut by low-cost suppliers trying to save on raw material.
Hole Diameter, Position, and Post Length
Every mounting hole needs a diameter, a position measured from a fixed reference edge, and a tolerance. Post length matters just as much: a rivet or logo pin that’s too short won’t clinch properly, while one that’s too long can crack the leather backing during installation.
For fixed hardware such as D rings and logo plates, post or pin length should exceed the combined thickness of the leather and lining by roughly 1-2mm to allow secure clinching without excess protrusion. Our D ring sourcing guide covers how wire diameter and hole spacing affect load capacity even when the outer ring size looks identical on paper.
Assembly Direction
Assembly direction tells the factory – and later the bag maker – which face is “up,” which side mounts against the leather, and how moving parts like turn locks or swivel hooks should orient once installed. Without this, symmetric-looking parts get assembled backward on the production line.
A simple arrow or a labeled front/back view on the drawing prevents this. For hardware with a functional moving part, such as a spring-loaded snap hook, indicate the open direction of the gate as well, since this affects how the part is used once it’s on the finished bag.
Surface Finish and Plating Color
Surface finish covers two separate things: the plating process and the color. State whether the part should be rack plated or barrel plated – rack plating suspends each piece individually for even coverage on visible parts, while barrel plating tumbles parts together and is more suitable for hidden or non-decorative components. Our rack vs barrel plating guide explains why this choice affects how a “gold” finish looks after a few months of handling.
Color should be referenced against a physical sample, a Pantone number, or an approved previous production batch – never a screen color, which shifts across monitors. Buyers selling into the EU should also confirm the plating chemistry meets REACH restricted-substance limits, since nickel release rules apply directly to metal hardware in prolonged skin contact.
Why Does the Same “Gold” Look Different Across Batches?
What: electroplated color depends on bath chemistry, plating time, and current density, all of which drift slightly over weeks of production. Why: two batches plated a month apart can show a visibly different gold tone even from the same factory line. How: request that all hardware for one collection be plated in a single run, and keep a signed physical color reference on file for every reorder.

🛠️ OEM/ODM Custom Hardware Solutions
Have a specific engineering drawing or custom design for luxury leather goods? Collaborate directly with our master engineers to transform your sketches into premium brass or zinc alloy components.
Start Your Custom Project →📂 Digital Product Catalog Access
Explore our comprehensive range of high-end handbag accessories, metal logo,turn locks, buckles, and chains. Download the full specifications and options catalog for your sourcing library.
Download Full Catalog ↓Logo Placement and Branding Details
Logo position, size, and depth need exact coordinates on the drawing, along with the presentation method: engraved, laser-marked, embossed, debossed, or enamel-filled. Each method produces a different visual result and a different cost, so specifying only “add our logo” leaves too much open to interpretation.
If the logo sits on a curved or beveled surface, note how the artwork should wrap or scale, since a flat logo file applied to a curved buckle face without adjustment often distorts. See our logo plate attachment guide for how pin placement on a logo plate interacts with leather thickness and mounting method.
Critical Dimension Tolerances
Not every dimension needs a tight tolerance, and marking all of them tight drives up cost without adding value. Reserve tight tolerances – typically ±0.05mm to ±0.1mm – for dimensions that affect fit and function: hole diameter, post length, and any surface that mates with another part.
Cosmetic dimensions such as overall length or decorative curve radius can usually carry a looser standard tolerance, often ±0.2mm to ±0.3mm for die-cast zinc alloy parts. Flagging every dimension as critical is a common mistake that slows down quoting, since the factory then has to price for full inspection on features that don’t actually need it.
How Should a Buyer Decide Which Dimensions to Tolerance?
What: only dimensions that affect assembly fit, strap or webbing width, or mechanical function should carry a tight tolerance callout. Why: over-toleranced drawings increase inspection time and rejection rates without improving the finished product. How: mark 3-5 critical dimensions per part with explicit tolerance values, and let the remaining dimensions follow the factory’s standard die-casting tolerance class.
Functional and Performance Requirements
Functional requirements describe what the part needs to do, not just what it needs to look like: load capacity for a D ring, closing force for a turn lock, or corrosion resistance for hardware headed to a coastal or humid market. These requirements should be written on the drawing as numbers, not adjectives.
Corrosion resistance is commonly verified through accelerated salt spray testing under the ASTM B117 standard. A practical baseline for moderate climates is 48 hours without red rust; humid or coastal markets often specify 72-96 hours. If the hardware carries daily load, state the expected static load in kilograms so the factory can confirm wire diameter and wall thickness against that number – our bag chain sizing guide shows how wire diameter changes load capacity even at identical link length.
Packaging Requirements
Packaging is easy to forget on a technical drawing, yet it affects cost and lead time just as much as the part geometry. Note whether hardware ships loose in poly bags, individually bagged with a header card, or bulk-packed by carton, and specify any anti-tarnish paper or desiccant needed for long ocean freight.
If hardware sets ship pre-matched – a buckle, D ring, and logo plate from the same plating batch, for example – state that requirement explicitly, since packaging by SKU rather than by set is the factory default unless told otherwise.
2D Drawing vs 3D CAD File vs Physical Sample
| Format | Best For | Limitation |
| 2D Technical Drawing | Standard buckles, plates, and rings with clear dimensions | Cannot fully convey complex curved surfaces |
| 3D CAD File (STEP/IGES) | Complex shapes, curved logo plates, ergonomic hardware | Requires mold engineering software to open and edit |
| Physical Sample | Color matching, texture reference, feel confirmation | Slower to ship and cannot capture internal wall thickness |
In practice, most OEM projects combine a 2D drawing for dimensions and tolerances with either a 3D file or a physical reference sample for shape and color. Relying on only one format usually leaves a gap somewhere in production.
Pros and Cons of Drafting Your Own Drawing
Pros:
- Full control over exact specifications before quoting begins
- Faster quote turnaround since the factory isn’t guessing at missing details
- Easier to compare quotes across multiple suppliers on an apples-to-apples basis
Cons:
- Requires basic CAD or drafting knowledge, or a designer on staff
- Small errors in hole position or tolerance can go unnoticed until sampling
- Doesn’t replace the need for factory engineering review before mold cutting
Common Mistakes in Hardware Drawings
- Leaving material and alloy grade blank, forcing the factory to default to the cheapest option
- Describing plating color in words only, with no physical or Pantone reference
- Omitting hole position tolerance, which is the leading cause of hardware that doesn’t align with pre-punched leather
- Marking every dimension as critical instead of flagging only the ones that affect fit
- Forgetting assembly direction on symmetric-looking parts
- Leaving packaging requirements out of the drawing and sending them separately, where they get lost
Factory Expert Tips
From our OEM production experience, the single change that improves first-sample accuracy the most is including a reference edge for every hole position measurement, rather than listing dimensions that assume the reader already knows where “zero” is. We also recommend sending a small strap or webbing sample alongside the drawing whenever a buckle or ring needs to thread through it – a $5 shipping cost on a fabric swatch is far cheaper than a mold revision after tooling is cut.
Factories that hold ISO 9001 certification typically run first-article inspection against the drawing before mass production, which catches most dimensional issues before they reach a full order. Ask your supplier to share this inspection report rather than just a pass/fail confirmation.
Expert Recommendation
When should you commission a full technical drawing? Any time the hardware is custom-molded, involves a logo, or needs to fit a specific leather thickness or webbing width, a complete drawing is worth the upfront time. For standard stock items ordered without modification, a shorter spec sheet referencing the factory’s existing part number is usually sufficient.
We generally advise against skipping the drawing entirely and relying only on a reference photo, even for simple shapes – photos don’t convey wall thickness, hole tolerance, or material grade, and those three gaps account for most of the rework we see on first-time OEM projects.

Conclusion
A complete bag hardware technical drawing is the fastest way to get an accurate quote and a first sample that matches expectations. Cover the twelve points above – dimensions, material, thickness, hole and post specs, assembly direction, finish, logo placement, tolerances, function, and packaging – and most sampling delays disappear before they start.
If you have a sketch, a reference sample, or even a rough idea and need help turning it into a production-ready drawing, our engineering team at custom OEM hardware manufacturing can build the full specification with you. You can also browse our current custom buckle hardware category for reference parts before starting a new drawing from scratch.
FAQ
What information does a factory need before quoting bag hardware?
At minimum, overall dimensions, material and alloy, wall thickness, hole specifications, and surface finish. Without these five items, any quote received should be treated as a rough estimate only.
Do I need a 3D CAD file or is a 2D drawing enough?
A 2D drawing is enough for simple, mostly flat parts like standard buckles or plates. Complex curved shapes, such as sculpted logo plates or ergonomic handle hardware, are better communicated with a 3D CAD file alongside the 2D dimensions.
How tight should tolerances be on a custom metal hardware drawing?
Functional dimensions such as hole diameter and post length typically need ±0.05mm to ±0.1mm. Cosmetic dimensions can usually carry a looser ±0.2mm to ±0.3mm tolerance for die-cast zinc alloy parts.
Can a factory create the technical drawing for me?
Yes. Most OEM hardware factories, including ours, offer drawing and mold engineering support starting from a sketch, reference sample, or rough description, though providing as much detail as possible upfront still speeds up the process.
What is the most commonly missed item on hardware drawings?
Assembly direction and hole position tolerance are the two most frequently missing items, and together they account for a large share of first-sample rejections.
Ready to source your handbag hardware?
Explore our full product range, request a custom quote, or reach out directly — we respond fast.