Bag Hardware Tolerance Explained: How Small Size Errors Affect Assembly
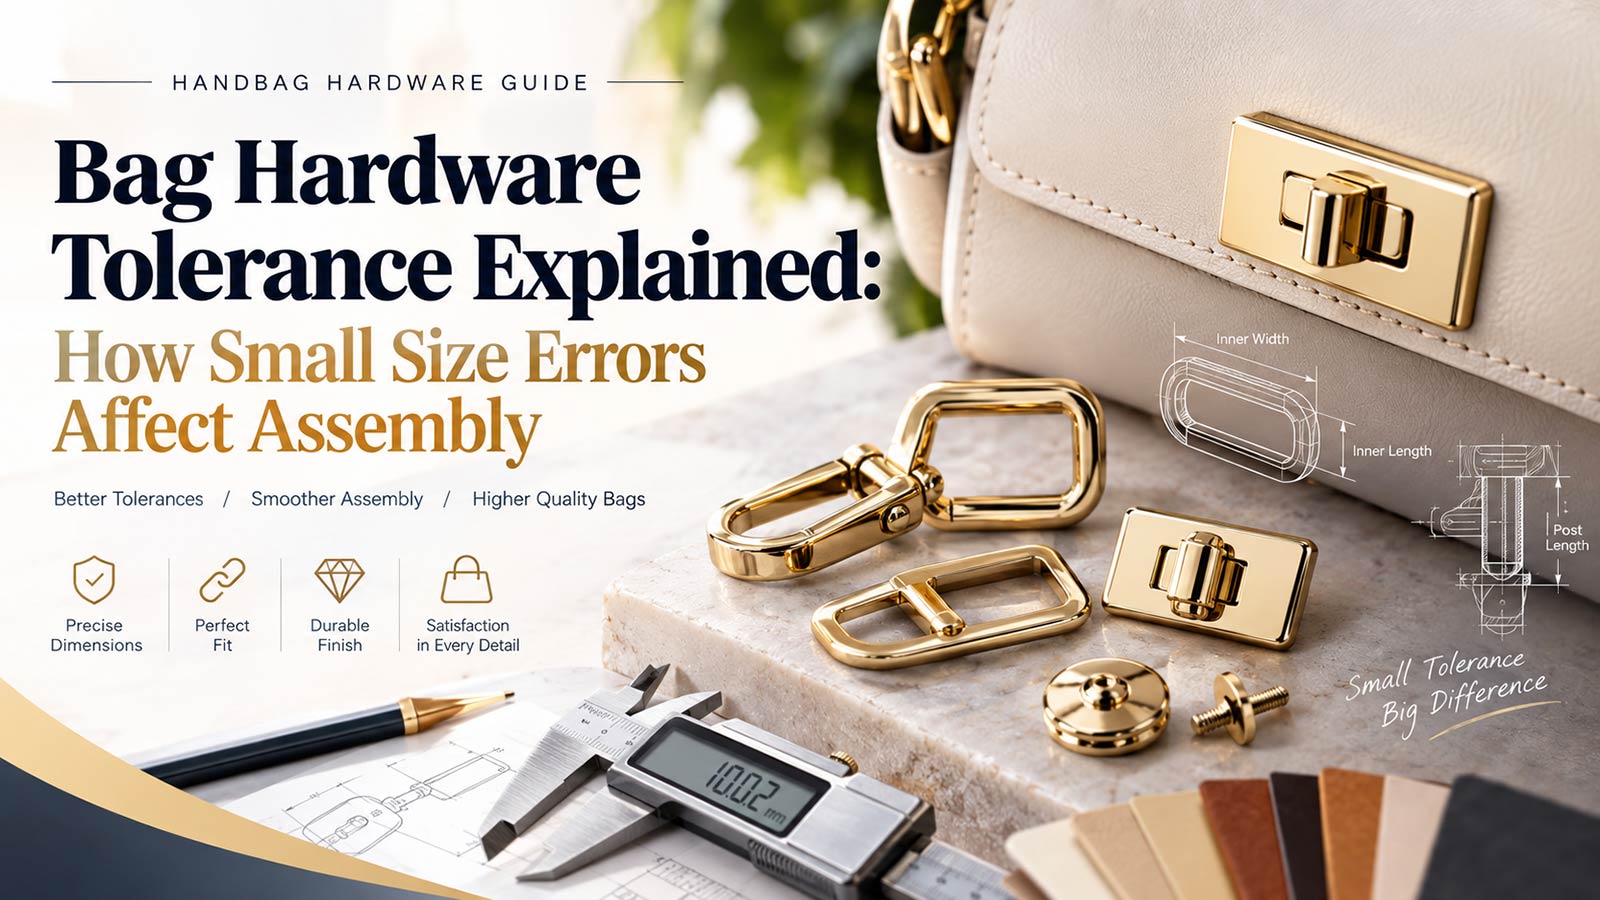
On a handbag production line, a turn lock that almost fits is more dangerous than one that clearly does not. A bag can pass every photo check and still fail in the customer’s hands: a strap ring that rattles, a lock that grinds, a post that never seats. In most of these cases the root cause is not the design. It is dimensional variation that nobody controlled at the drawing stage.
This guide explains how bag hardware tolerance works, which dimensions decide whether a lock, ring or buckle assembles cleanly, and how electroplating quietly changes the final size of every plated part.
Quick Answer
Bag hardware tolerance is the allowed difference between a part’s real dimensions and the values on its technical drawing, and even a small dimensional difference can affect how hardware fits, rotates or locks. Industry die-casting design data puts typical variation for small zinc alloy features in the tenths-of-a-millimetre range, while decorative electroplating adds a measurable metal layer per surface. Assembly problems start when hole-to-pin clearance, post length, body thickness and left/right pairing are not specified as mated dimensions.
Key Takeaways
- Specify tolerances on mated dimensions such as pin and hole, or post and leather stack, not on every measurement on the drawing.
- Zinc die casting can hold tenths-of-a-millimetre accuracy on small features formed in one die half; dimensions across the parting line are wider.
- Electroplating adds metal: external surfaces grow, holes and threads shrink. Measure finished, plated parts, not raw castings.
- Left and right hardware pieces are a mated pair. Tolerancing them as two independent parts is a common cause of binding locks.
- A 48 to 96 hour salt spray test is a useful plating screen, but it never replaces a physical fit check on real leather.
Table of Contents
- What Is Bag Hardware Tolerance?
- The Dimensions That Control Assembly Fit
- How Small Errors Break Assembly
- How Plating Changes Final Dimensions
- Typical Tolerance Ranges for Zinc Alloy Hardware
- Tight vs Standard Tolerances: Pros and Cons
- Common Mistakes Buyers Make
- Factory Expert Tips
- Expert Recommendation
- Conclusion
- FAQ
What Is Bag Hardware Tolerance?
Tolerance defines how far a real part may drift from its drawing without failing its job. For handbag hardware, the drawing states a nominal dimension, such as a 32 mm inner ring length, and the tolerance states the allowed band around it. Two parts can both be inside their own tolerance and still behave differently on the same bag.
That is why fit must be engineered between parts, not measured on one part in isolation. A pin and its hole each carry a tolerance; the assembly only works when the gap between them is controlled as a pair.
Knowledge Box: Tolerance vs Fit
What: Tolerance is the allowed variation of one dimension; fit is the working relationship between two mated dimensions, such as a pin and its hole. Why: A pin and a hole can each pass inspection and still wobble or seize, because their errors add together. How: Define fit as a clearance target, for example a minimum and maximum gap between pin diameter and hole diameter, and control both parts to protect it.
The Dimensions That Control Assembly Fit
Four groups of handbag hardware dimensions decide whether a fitting assembles cleanly: hole and ring inner dimensions, pin and post lengths, body thickness and edge condition, and the relationship between left and right pieces. If any one of them drifts, the symptom appears at assembly or, worse, after a month of daily use.
Hole Diameter and Ring Inner Dimensions
Pins, hook gates and strap loops all pass through openings. If a cast hole runs small, or a ring inner width shrinks after plating, a hook gate may not clear the opening or a folded strap will pinch inside the ring.
Pin and Post Length
Post length sets how deeply a lock or logo plate seats through the leather. Too short, and the receiver never engages; too long, and the post pushes through the lining or forces the lock face to stand proud of the leather.
Body Thickness and Edge Condition
Thickness controls the visual gap between the lock and the leather surface, plus the clamping force of screws and rivets. Edge radius matters too: a radius that is too small after polishing can cut into a strap over time.
Left and Right Pairing
Many fittings, such as lock bodies, hinge lugs and strap connectors, exist as mirrored left and right versions. A left part produced at one end of its tolerance band and a right part at the other end can look perfectly matched yet bind when assembled.
To see how these dimensions are documented in practice, review the 32mm rectangular strap ring technical drawing, which labels inner length, inner width and thickness as separate controlled dimensions.
How Small Errors Break Assembly
Every assembly symptom on the line maps back to one or two dimensions. The decision table below connects what assemblers see to the dimensional cause, which makes it useful both for rejecting goods and for revising a drawing before mold cutting.
| Assembly Symptom | Likely Dimensional Cause | Check on Drawing | Typical Fix |
|---|---|---|---|
| Wobble or rattle in ring or hook | Hole-to-pin clearance too large | Pin diameter and hole diameter, toleranced as a pair | Tighten the fit or add a spring element |
| Lock grinds or will not rotate | Hole small after plating, or post position offset | Plated hole diameter and post location | Size the hole before plating; jig the post position |
| Post pushes through lining | Post long, or leather stack underestimated | Post length vs leather plus reinforcement thickness | Shorten post or specify the full stack |
| Strap pinches inside ring | Ring inner width below folded strap thickness | Inner width vs folded strap and edge-paint stack | Widen the inner dimension |
| Left and right lock halves bind | Paired parts at opposite ends of their bands | Left and right features controlled as a mated set | Paired inspection and matched tolerancing |
| Screws strip or work loose | Boss hole off-size after plating; short engagement | Thread specification plus plating allowance | Tap after plating; countersink the lead-in |
All values in this guide are in millimetres. Tolerance figures quoted from industry sources are total bands unless marked with a plus-minus sign. The “typical fix” column is general engineering guidance, not a DG Buddy test result.

View our product catalog
Download our complete handbag hardware catalog with full specs, finishes, and minimum order details.
⬇ Download catalogGet in touch with us
Have questions about pricing, MOQ, or lead time? Our team is ready to assist with your sourcing needs.
→ Contact usKnowledge Box: Tolerance Stack-Up
What: Tolerance stack-up is the accumulation of variation from every part in an assembly chain, such as lock body, leather, reinforcement plate and back plate. Why: Each part can be inside its own tolerance while the chain grows too long or too short overall. How: Add the bands of every stacked dimension and compare the worst case with the post length. If the worst case fails, redesign the chain, not just one part.
How Plating Changes Final Dimensions
Electroplating does not colour the metal. It adds metal. A decorative copper-nickel-chrome stack typically deposits on the order of 10 to 30 micrometres per face depending on the recipe, and the deposit is not uniform. It builds up on convex edges, tips and corners, while holes, threads and recesses receive less.
For hardware, that means the hole you cast is not the hole you ship. Internal diameters shrink, external diameters grow, and threaded lead-ins can partially close. Published zinc die-casting plating guidance recommends rounding edges, avoiding very small blind holes, and countersinking threaded holes precisely so plating does not destroy the assembly function.
Rack plating, where parts hang on fixtures, gives the most uniform deposit on visible pieces but costs more. Barrel plating, where small parts tumble together, is cheaper and faster but leaves contact marks and is usually reserved for small, durable components rather than lock faces.
One practical consequence: critical dimensions should be measured on plated, finished parts. A caliper check on raw castings only confirms the die. Only a post-plating check confirms the part that actually ships.
Knowledge Box: Why Holes and Threads Suffer Most
What: Electroplate distributes unevenly: thick on projections, thin in recesses. Why: Plating current concentrates where electrical resistance is lowest, so external corners grow fastest while deep holes and threads are starved. How: Industry design rules advise a generous edge radius, holes at least about 5.6 mm where full plating coverage is required, and tapping threads after plating when guaranteed engagement matters.
Typical Tolerance Ranges for Zinc Alloy Hardware
Zamak, the zinc alloy family used for most die-cast bag hardware, is among the most precise net-shape processes available to factories, but its capability depends on which die feature forms the dimension. The ranges below come from published industry design data from the International Zinc Association and North American die-casting practice, not from a single factory’s test report. Treat them as negotiation starting points.
| Reference Level | Scope | Value | Basis | Buyer Note |
|---|---|---|---|---|
| Economic, one die half | 0 to 25 mm features | 0.10 mm | Total band | Lowest cost, first-trial dies |
| Standard, first trial | General dimensions | 0.2% of dimension plus 0.1 mm | Total band | Achieved without die adjustment |
| Best achievable | Precision features | 0.1% of dimension | Total band | Needs SPC and die correction trials |
| Across the parting line | Same size range | 0.26 to 0.70 mm | Total band | Wear between die halves adds variation |
| Decorative plating stack | Per plated face | 10 to 30 micrometres (recipe-dependent, estimate) | Approximate | Adds to external size, shrinks holes |
Read the table this way: a 20 mm pin formed in one die half carries roughly a 0.10 mm total band at the economic level, or about 0.05 mm per side, before plating. The same pin formed across the parting line can drift several times further, which is why critical pins should be designed into one die half wherever possible. For the full feature-by-feature data, see the zinc die-casting design rules and tolerance tables.
Tight vs Standard Tolerances: Pros and Cons
Tight tolerances are not automatically better. They are a purchasing decision with a real cost attached, and the right level depends on which failure mode you are protecting against.
Pros of tighter tolerances: a consistent snap and lock feel, interchangeable parts during repair, less rework at the bag factory, and a more premium tactile quality.
Cons of tighter tolerances: higher die maintenance and inspection cost, longer sampling cycles, more scrap when the process drifts, and wasted money when applied to dimensions that do not affect assembly.
Pros of standard economic tolerances: lower tooling and inspection cost and faster first trials. Cons: fits must be engineered with more designed-in clearance, assembly may need more adjustment, and a loose fit can turn into rattle if clearance is not deliberately planned.
Common Mistakes Buyers Make
- Tolerancing every dimension. Walls of tolerances on non-critical features inflate cost and inspection load. Protect the five or six dimensions that control fit.
- Measuring raw castings instead of plated parts. The part that ships is plated. If your approval sample was measured before plating, your limits are wrong.
- Ignoring plating in hole and thread dimensions. Holes shrink and threads tighten after the line. Size them with a plating allowance or tap after plating.
- Treating left and right pieces as independent parts. Mirrored fittings need paired tolerancing and paired inspection, or they will eventually bind.
- Approving the lock, ring and strap separately. Hardware is a system. Test it assembled on real material, the same system logic used when building a matching handbag hardware set.
Factory Expert Tips
From OEM production experience, the most reliable habit is to lock the “mated dimensions” list with the engineer before the mold is cut: every pin and hole pair, every post length against the real leather stack, every ring inner width against the folded strap thickness. Fixing these on paper costs nothing; fixing them after mold trials costs weeks.
Ask for a gauge plan with the sample. Go/no-go plug gauges for holes, caliper check points for posts, and retained golden samples let the bag factory verify fit without a measuring laboratory. A quality system audited against ISO 9001 makes this documentation more consistent between sample and bulk.
Use salt spray testing as a screen, not a verdict. DG Buddy offers 48 and 96 hour salt spray testing on plated parts using the ASTM B117 salt spray practice, which compares coating behaviour under controlled fog. It is one quality input alongside adhesion and fit checks, and for disputed shipments a third-party laboratory such as SGS testing services can re-test against the same criteria.
Finally, validate the sample on the real assembly. A lock that snaps perfectly on bare metal can still fail on a thick, reinforced flap. For a view of how sampling, inspection and approval connect, see DG Buddy’s custom handbag hardware manufacturer service overview.
Expert Recommendation
Specify tight, paired tolerances on functional interfaces, such as locks, hinges and posts, and standard economic tolerances everywhere else when production volume justifies die maintenance and the brand promise depends on tactile quality. Keep one factory responsible for the mated set so errors cannot be passed between suppliers. Write the custom hardware tolerance plan as paired dimensions on the drawing itself, not as a footnote in an email thread.
Do not over-specify. For first collections, small test runs or simple decorative parts, use standard tolerances with deliberately engineered clearance and a 100 percent assembly check at the bag factory. The decision boundary is the failure mode: if a dimension failing makes the bag look imperfect, standard tolerance is fine; if it makes the bag unable to close or the strap detach, specify the fit as a paired dimension. Plan one sample round to prove it, using a realistic custom hardware sample timeline that includes plated-part measurement.

Conclusion
Bag hardware tolerance is not an abstract engineering nicety. It is the difference between a lock that snaps cleanly for five years and one that grinds on the first day. Start every hardware brief from the assembly, not the part list: write down every mating pair, decide the clearance you want, then set tolerances that protect that clearance through casting, polishing and plating.
If you are preparing a drawing, DG Buddy’s engineers can review tolerance and plating fit before mold cutting. Send your drawing for an OEM engineering review, or explore the factory’s hardware range on the DG Buddy homepage to shortlist components for your next collection.
FAQ
What tolerance can zinc alloy bag hardware realistically hold?
For small features up to about 25 mm formed in one die half, published industry design data gives a total band around 0.10 mm at the most economical level, with tighter results possible using process control. Dimensions across the die parting line are wider. Always confirm capability for your specific geometry with the factory before fixing the drawing.
Does electroplating change the size of holes and threads?
Yes. A decorative plating stack adds a measurable layer per face, growing external surfaces and shrinking internal ones. Threads and small holes are the most exposed because plating deposits unevenly. Design countersinks, allow plating thickness in the dimension, or tap threads after plating.
Which bag hardware dimensions cause the most assembly failures?
In factory experience the repeat offenders are pin-to-hole clearance, post length versus the real leather stack, ring inner width versus folded strap thickness, and left-to-right pairing on mirrored parts. Each of these should be specified as a mated dimension pair, not as two independent measurements.
How should I measure hardware for a technical drawing?
Use a digital caliper on plated, finished samples, and record minimum and maximum values across a batch of at least 30 pieces. State clearly on the drawing whether each dimension applies before or after plating, because the factory will otherwise assume the cheaper interpretation.
What salt spray test hours should I specify for plated hardware?
A 48 to 96 hour exposure is a common screening range for fashion hardware, agreed per finish and use case. ASTM B117 defines how the test is run; it compares coatings under the same fog conditions but does not by itself predict years of service. Combine it with adhesion checks, fit checks and, for critical orders, third-party verification.
Ready to source your handbag hardware?
Explore our full product range, request a custom quote, or reach out directly — we respond fast.