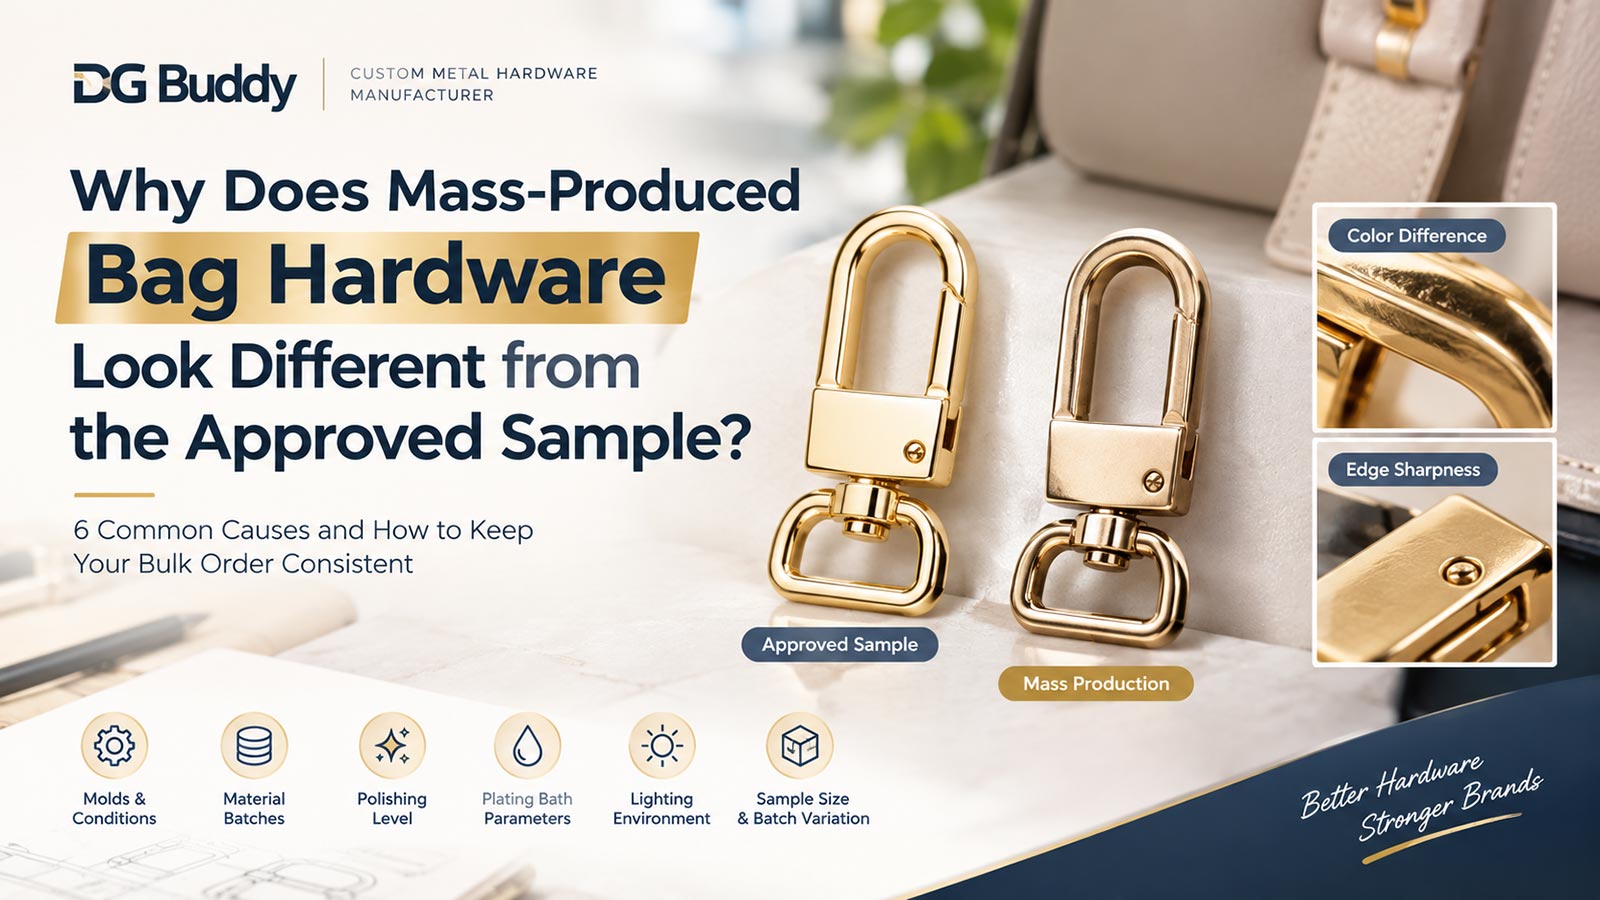
Why Does Mass-Produced Bag Hardware Look Different from the Approved Sample?
Introduction
A buyer approves a beautiful sample, then opens the bulk carton and finds the gold looks warmer, the logo edge softer, or the weight slightly off. This is the classic case of mass production hardware different from sample, and it rarely comes from one mistake. Usually several small, normal manufacturing variables add up.
The good news is that most of these variables can be measured and controlled before the order starts. This guide explains six real causes of bag hardware sample variation, shows which ones a buyer can influence, and gives a practical plan for tighter matching, building on our pre-production sample approval checklist.
Quick Answer
Bulk bag hardware looks different from the approved sample because a sample is a small, closely supervised run, while mass production uses production molds, new material batches, machine polishing, shared plating baths and different lighting. Reduce the gap by sealing a golden sample, defining limit samples for color and gloss, locking the plating method, checking under standard light, and approving a pre-shipment sample from the real run.
Key Takeaways
- Some variation is normal; what matters is whether it stays inside a written, agreed tolerance.
- Six drivers explain most gaps: molds and production conditions, material batches, polishing, plating bath parameters, lighting, and too few sample pieces.
- Color is the most disputed attribute, so judge it against a physical reference under standard light, never on a screen.
- The plating method (rack or barrel) and recorded bath settings matter more than the color name on the purchase order.
- Approve a sealed golden sample plus light and dark limit samples before releasing bulk production.
- Ask for a pre-shipment sample from the actual production run, with plating batch codes.
Table of Contents
- Introduction
- Quick Answer
- Key Takeaways
- Mass Production Hardware Different From Sample: What Is Really Happening
- 1. Molds and Production Conditions Are Not the Same
- 2. Raw Material Batches Change
- 3. Polishing Level Shifts From Sample to Bulk
- 4. Plating Bath and Process Parameters Drift
- 5. Hardware Color Difference Under Different Lighting
- 6. A Small Sample Cannot Show Batch Fluctuation
- Causes, Symptoms and Controls at a Glance
- How to Reduce Color Difference in Custom Bag Hardware: 7 Steps
- Pros and Cons of Adding Limit Samples
- Common Mistakes
- Factory Expert Tips
- Expert Recommendation
- Conclusion
- FAQ
Mass Production Hardware Different From Sample: What Is Really Happening
A sample and a bulk order are made under different conditions, so some difference is expected. The practical question is not whether they match perfectly, but whether the gap sits inside a tolerance both sides agreed in writing. A visible mismatch usually means one of six variables moved, or the approval never defined how much movement was acceptable.
It helps to separate three kinds of variation. Dimensional drift affects fit, finish variation affects color and gloss, and structural variation affects weight and function. This article focuses on finish and appearance, because that is where most complaints begin. Custom hardware color difference is also the hardest to settle after shipment, since each side remembers the sample differently.
1. Molds and Production Conditions Are Not the Same
Molds and production conditions change first, because a sample is often made while the process is still being tuned. Once bulk starts, the shop runs a production mold at stable but different settings. Small shifts in die temperature, injection pressure or cycle time can alter surface texture, parting lines and edge sharpness before any plating is applied.
Mold condition also matters over time. DG Buddy’s handbag hardware production process guide notes that trial runs are used to tune casting parameters, and that a neglected mold can cause dimensional drift. A multi-cavity mold can also give slightly different parts from each cavity, which a handful of samples may hide.
Consider a common manufacturing scenario. A prototype cut by CNC or made from a temporary tool can look sharper than a die-cast part from the production mold. That is not a defect, but the buyer should be told how the sample was made, so the approval reflects the real process.
2. Raw Material Batches Change
Raw material batches change because zinc alloy ingots, brass stock and stainless steel are bought in lots, and each lot carries its own certificate. Composition stays inside the grade limits, yet small differences can influence casting behavior, surface porosity and plating adhesion. Those effects can appear as a slight shift in tone or gloss after finishing.
A more serious risk is substitution. Swapping in a cheaper alloy, or a different Zamak grade, without notice is a recognized way for sample quality to slip during scale-up. A lighter part also often means thinner walls, which affects both perceived quality and plating durability. Weight is therefore a fast, useful check. Ask for the alloy grade, incoming material records and batch traceability in writing, and record the approved sample’s weight as a reference point.
3. Polishing Level Shifts From Sample to Bulk
Polishing is the step buyers underestimate most. Grinding and polishing prepare the surface for plating, and plating copies whatever it sits on: a mirror surface stays bright, a satin surface stays soft. If bulk polishing is less complete or more aggressive than on the sample, final gloss and edge sharpness will not match.
Polishing uses both machines and skilled hands. In a common manufacturing scenario, an experienced worker gives a sample extra attention on every edge and recess, while a bulk run shares the work across tumbling, wheels and several operators. Roughness targets help: DG Buddy’s production guide cites Ra 0.4 μm or lower for mirror finishes and 0.4–0.8 μm for satin.
Pre-plating inspection matters just as much. Electroplating cannot truly cover pits, pinholes or polishing dead zones, and it often makes them more visible. A defect missed before plating becomes a visible defect after it.
4. Plating Bath and Process Parameters Drift
Plating is where most color complaints originate. Electroplating deposits metal from a chemical bath, and the result depends on bath chemistry, temperature, current, plating time and bath age. The plating shop adjusts these settings continuously, so the sample batch and the bulk batch may not be plated under identical conditions.
Colors such as light gold, gunmetal and antique finishes are especially sensitive. DG Buddy’s guide to rack plating explains that finer control over voltage, time and solution balance is essential for these colors. Plating batch variation also means parts from separate batches can look mismatched once assembled side by side, even if each piece passed inspection alone.
Knowledge Box: Rack Plating vs Barrel Plating
What: Rack plating hangs each part on a fixture, while barrel plating tumbles many parts together in a rotating drum. Why: Racked parts receive more controlled current and avoid part-to-part contact, so color and edges stay more consistent. Barrel plating is faster and cheaper, but can leave micro-scratches and uneven thickness on edges. How: For visible hardware, confirm in writing that bulk will use the same method as the approved sample.
5. Hardware Color Difference Under Different Lighting
Lighting changes color judgment because metal finishes reflect the light source around them. A sample photographed under warm factory bulbs and a carton opened under cool office LEDs can look like two different golds. Screens add another variable through brightness and calibration, which is why photo approval is unreliable for plated finishes. Hardware color difference under different lighting is one of the most common causes of false alarms and false approvals.
Knowledge Box: Metamerism and Standard Light
What: Metamerism is when two surfaces match under one light source and differ under another. Why: Plating, lacquer and base metal reflect wavelengths differently, so a pair that agrees in the factory can disagree in a showroom. How: Compare sample and bulk side by side, at the same angle, under one standard light. DG Buddy’s inspection guide describes D65 daylight at about 1,000–1,500 lux for appearance checks.
Numbers can support the eye. Color difference is often expressed as ΔE, and the CIEDE2000 colour-difference formula was designed to correlate better with perceived differences. However, highly reflective metal needs care, so agree the instrument, geometry and gloss handling first. No universal ΔE limit fits every finish, and visual comparison under standard light should remain the final check.
6. A Small Sample Cannot Show Batch Fluctuation
A small sample cannot show batch fluctuation because it captures a few pieces from one moment. Bulk production runs thousands of pieces across shifts, bath conditions and material lots, so it produces a spread of results. Judging that spread from three or five pieces is like judging a season from one afternoon’s weather.
Testing standards recognize the same problem. ASTM B117, the salt spray test practice, states that reproducibility depends on the specimens and evaluation criteria, and that enough replicates should be included to establish variability. Appearance works the same way: you need several pieces, ideally from more than one run, to see the true range.
Time adds to the gap. According to our custom hardware sample timeline guide, an approved sample typically takes 10–20 working days, and our production guide adds 15–25 days for mass production. Over those weeks, bath age, material lots and operators can all change.

Browse the hardware catalog
Download our full product catalog to explore styles, materials, and specifications for all hardware collections.
⬇ Download catalogCustom OEM manufacturing
Need a unique design? We offer full OEM customization — your logo, finish, and specifications on any hardware.
→ Learn about OEMCauses, Symptoms and Controls at a Glance
Use this table to decide what to lock before bulk starts. Read it from the right-hand columns backward: first choose the evidence you want to see, then confirm the control that produces it. The entries are qualitative and based on common manufacturing scenarios and DG Buddy production guidance, not measured data.
| Cause | Typical visible symptom | Control to lock before bulk | Evidence to request |
|---|---|---|---|
| Mold and production conditions | Softer edges, different texture or parting lines | Same production mold and process route as the sample | First-piece photos and dimensions from the production mold |
| Material batch | Slight tone or weight change | Named alloy grade, no substitution | Material certificate, batch traceability, piece weight |
| Polishing | Duller or over-rounded surface | Written gloss level and roughness target | Pre-plating inspection photos |
| Plating bath and parameters | Warmer, cooler or darker color | Same plating method; reuse recorded sample parameters | Plating batch codes, thickness report |
| Lighting | “Looks different” only in some places | One standard light for all checks | Side-by-side photos under D65 daylight |
| Small sample size | Bulk range wider than the sample suggested | Limit samples and a golden sample | Pre-shipment samples from the real run |
Two rows deserve extra attention. Plating and lighting cause the most disputes, yet both are cheap to control with a written method and a standard viewing condition. Mold and material changes are rarer but costly, so ask the factory to disclose any change in route before production, not after.
How to Reduce Color Difference in Custom Bag Hardware: 7 Steps
To reduce color difference in custom bag hardware, accept first that variation cannot be removed, then narrow it and define what is acceptable. These seven steps work for most orders, and they cost far less than a rejected shipment. Start them at the sample stage, because every step is easier to agree before tooling and plating are locked.
- Seal a golden sample. Mark one approved piece as the reference and keep a duplicate with the supplier, so both sides measure against the same object.
- Define limit samples. Approve the lightest and darkest acceptable pieces, plus a gloss limit, so inspectors see the tolerance rather than debate it.
- Write the finish specification. State the base metal, plating method, layers, topcoat, gloss level and minimum thickness, not just a color name.
- Confirm the production route. Ask whether the mold, alloy, polishing and plating line match those used for the sample, and request disclosure of any difference.
- Standardize viewing. Agree one light source, one angle and side-by-side comparison, and ignore screens and phone photos for final decisions.
- Request a bulk pre-shipment sample. Ask for pieces from the finished run, with plating batch codes, and keep matching sets from the same batch.
- Agree inspection rules. Define AQL levels and which color or gloss deviations count as major defects before production starts.
This is also how to match plating color in mass production: record the sample’s plating parameters and reuse them. Close matching is achievable when sample parameters are documented and reapplied, though very small natural variation between batches remains normal.
Knowledge Box: Golden Sample for Bag Hardware
What: A golden sample for bag hardware is the approved, sealed piece that becomes the physical standard for production and inspection. Why: It removes memory and screen differences from disputes. A limit sample adds the acceptable range around it, because one piece shows the target but not the tolerance. How: Seal and date the golden sample, store it away from handling and humidity, and keep a matching copy at the factory.
Pros and Cons of Adding Limit Samples
Limit samples turn a vague “close enough” into a visible range that inspectors, buyers and factory staff can all hold in their hands. They are not free, so weigh the benefits against the extra sampling work before adding them to every order.
Pros
- Inspectors compare against a physical range instead of opinions.
- Disputes are settled faster because both sides hold the same reference.
- The supplier knows how much plating or polishing variation is acceptable.
Cons
- Producing and shipping extra pieces adds sample time and cost.
- Limits set too loosely can legitimize a visible mismatch.
- Reference pieces can tarnish or scratch if stored carelessly.
Common Mistakes
- Approving from photos or video. Lighting and screen settings can make an off-tone finish look correct.
- Naming a color but not a method. “Light gold” without a plating method, layers and gloss level leaves too much open.
- Having no written tolerance. Without it, any visible gap becomes an argument rather than a measurement.
- Splitting a collection across batches. Locks, buckles and logo plates plated in different runs may not match when assembled.
- Checking under a warm bulb. A single office or workshop light can hide or exaggerate a difference.
- Ignoring weight. A lighter bulk piece can signal thinner walls or a different alloy.
Factory Expert Tips
From OEM production experience at DG Buddy, even when each piece passes inspection on its own, plating batches can vary, so finishes should be checked again once the pieces are assembled together. Keep every visible part of one bag set in the same plating run whenever the schedule allows.
Record the plating parameters at the sample stage and reuse them for bulk, because that is the most reliable path to close matching. Buyers who also send real leather or webbing offcuts get first samples closer to production reality, and requesting salt spray or compliance documents during sampling avoids a costly conversation after tooling is locked.
A final practical point: reorders placed months later are unlikely to be plated in the same bath, so ask for a fresh pre-shipment sample each time and compare it with the sealed golden sample.
Expert Recommendation
Use the full control set (golden sample, limit samples, written finish specification and pre-shipment sample) when hardware is highly visible, finished in light gold, gunmetal or antique, or sold as a matching set. These are the situations where small shifts in plating or polishing are noticed immediately by customers.
A lighter process is acceptable for hidden parts such as internal rivets or screws, where a standard tolerance and a spot check are enough. It is not recommended to approve any visible finish from a photo alone, or to release bulk without a written agreement on what counts as an acceptable difference.

Conclusion
Mass production hardware different from sample is usually the result of normal variables, not negligence: molds and process settings, material lots, polishing, plating baths, lighting and small sample size. Each can be measured, written down and controlled if the buyer asks early.
If you want a second opinion on your sample, finish specification or tolerance wording, review our custom OEM hardware service or contact the DG Buddy team with your drawings and reference pieces.
FAQ
Is some color difference between sample and bulk hardware normal?
Yes. Very small natural variation between plating batches is normal, even with good control. The goal is to keep it inside a written tolerance, supported by a golden sample and limit samples, so that any visible shift can be judged against an agreed range.
How many sample pieces should I approve?
There is no universal number, but one piece is rarely enough. Approve a sealed golden sample plus light and dark limit samples, and ask for several pieces from the real production run before shipment, so you can see the actual spread.
Can a factory match the sample color exactly?
Not exactly in every piece. A factory can match closely by reusing recorded sample parameters, the same plating method and the same materials. Expect a small range around the target, and define that range in writing before production begins.
Does rack plating guarantee identical color?
No. Rack plating gives tighter control over current and part contact, so it usually produces more consistent color and cleaner edges than barrel plating. Bath conditions and batches can still differ, so you should still verify with batch codes and a pre-shipment sample.
Should I approve hardware from a photo or video?
Photos help for a first look, but they should not approve color. Lighting and screen settings can make an off-tone finish look acceptable. Confirm color, weight and function against the physical piece under standard light before releasing the order.
What should I do if bulk hardware does not match the sample?
If bulk hardware does not match the sample, compare the pieces with the golden sample and written specification under the same standard light, then photograph them side by side. Check plating batch codes and weight, and send the supplier the evidence. A clear written reference makes correction or replating much easier to agree.
Ready to source your handbag hardware?
Explore our full product range, request a custom quote, or reach out directly — we respond fast.